2026 Top Column And Boom Welding Machine Types?

Time:2026-09-14 Author:Ethan
0%

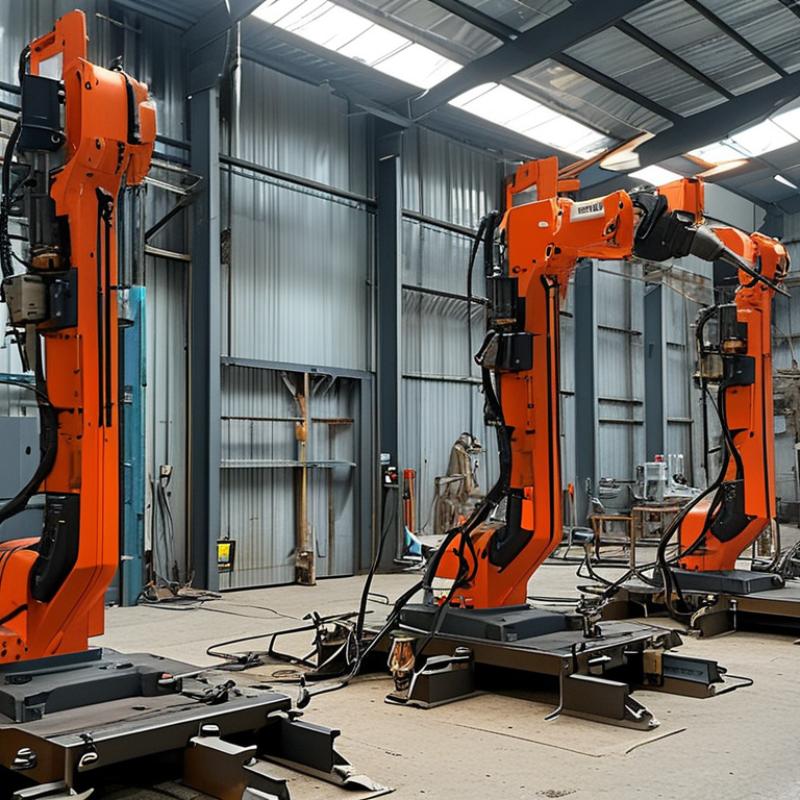
Choosing the right Column And Boom Welding Machine in 2026 requires more than comparing reach, load capacity, and price. Manufacturers now handle larger vessels, structural frames, pressure components, and irregular assemblies with tighter quality expectations. The machine must fit the workshop, not merely look impressive in a catalog.

Common types include fixed column and boom systems, traveling models, rotating designs, and compact machines for limited floor space. Each type solves a different production problem. A fixed system can offer stable positioning for repeated welds. A traveling model can cover longer workpieces without repeated repositioning. Rotating systems may improve access around cylindrical parts, while compact designs help smaller fabricators protect valuable floor area.

Real workshop experience shows that capacity figures do not tell the whole story. Cable routing, operator visibility, torch alignment, maintenance access, and control response can strongly affect daily output. A powerful machine can still perform poorly when its boom movement feels rough or its controls are difficult to adjust. That detail is easy to miss.

This guide examines the leading Column And Boom Welding Machine types expected to attract attention in 2026. It compares their structures, welding applications, automation features, and practical limitations. The discussion also considers safety controls, service support, fixture compatibility, and long-term reliability. No single design is perfect. The best choice depends on weld length, component geometry, production volume, and available budget. A careful buyer should verify specifications with real workpieces before making a final decision.
2026 Top Column And Boom Welding Machine Types?

2026 Column-and-Boom Welding Machine Classes by Boom Reach and Load Capacity

2026 Top Column And Boom Welding Machine Types?

In 2026, column-and-boom welding machines are best compared by boom reach and load capacity. These two factors affect weld access, torch stability, floor layout, and production speed. The classes below are practical engineering bands, not a universal international standard.

Light-duty machines usually provide 2–4 meters of reach and support 250–500 kilograms of welding equipment and tooling. They suit tanks, beams, and medium fabrication cells. Medium-duty units commonly reach 4–8 meters and carry 500–2,000 kilograms. They fit longer vessels and automated circumferential welding. Heavy-duty machines may extend 8–12 meters, with capacities from 2–10 tonnes. Extra-heavy systems exceed 12 meters and support more than 10 tonnes, but foundation design becomes critical. The boundaries are not perfect.

The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. That growth supports greater demand for repeatable welding motion and integrated sensing. However, reach alone does not define productivity. Buyers should verify vertical travel, boom deflection, duty cycle, rail accuracy, and emergency stopping performance. AWS D1.1 remains a useful reference for structural welding quality, although it does not classify machines by reach. In practice, a longer boom can reduce repositioning, yet it may increase vibration and alignment errors. That trade-off is easy to underestimate. Load ratings also need careful checking. A rated capacity may cover the carriage and torch, not the workpiece or fixture. Procurement teams should request load charts, tested deflection data, and site-specific foundation calculations.

2026 Column-and-Boom Welding Machine Classes by Boom Reach and Load Capacity

The chart presents practical engineering specification bands for column-and-boom welding machines. Boom reach is shown in meters, while rated load capacity is shown in metric tonnes. Light-duty machines are commonly used for smaller vessels and structural parts, while heavy-duty and extra-heavy-duty systems support longer weld seams, larger workpieces, and higher fixture loads. Values represent typical specification ranges and are not company or brand data.

Submerged Arc Systems: Comparing 5–15 kg/h Deposition Rates by Type

2026 Top Column And Boom Welding Machine Types?

Submerged arc systems are often compared by deposition rate, but wire configuration changes the result sharply. A single-wire column and boom machine typically deposits about 5–9 kg/h under stable production conditions. This range reflects guidance in the American Welding Society’s Welding Handbook, which links output to current, wire diameter, flux, and duty cycle.

Twin-wire systems commonly reach 8–13 kg/h. They suit long fillet welds and heavy plate, where arc stability matters more than rapid repositioning.

Tandem-wire systems can approach 12–15 kg/h in favorable trials, according to productivity data discussed by the International Institute of Welding. However, the upper figure is not automatic. Joint preparation, travel speed, and flux recovery can reduce real output.

Strip-electrode submerged arc equipment offers broad coverage for corrosion-resistant layers. Its deposition rate may sit near 8–15 kg/h, depending on strip width and welding current. Column stiffness also matters. Vibration can create uneven beads, even when the power source looks adequate.

Field experience exposes a common weakness: catalog rates rarely equal finished weld output. A practical estimate should subtract setup time, slag removal, inspection, and repositioning. Some figures wobble.

For a 5–15 kg/h target, single-wire equipment favors controlled, flexible work. Twin-wire and tandem designs favor long seams and higher utilization. The best selection depends on joint length, plate thickness, and required penetration—not deposition rate alone.

Fixed, Traveling, Rotating, and Tandem-Arc Machine Configurations

2026 Top Column and Boom Welding Machine Types

Fixed, traveling, rotating, and tandem-arc configurations serve different production realities. A fixed column and boom suits repeatable welds at one station, such as longitudinal seams on vessels. Its rigid layout simplifies programming and improves torch stability. A traveling machine moves along rails, covering long welds without repeatedly repositioning the workpiece. This matters for beams, tanks, and large structural assemblies.

Rotating configurations turn the workpiece while the boom maintains a controlled welding position. They can reduce awkward torch angles and support consistent circumferential welds. Tandem-arc machines use two coordinated wires, increasing deposition potential on thick sections. However, higher output can also raise heat input, distortion, and parameter sensitivity. More speed is not always better.

The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023, according to World Robotics 2024. That figure signals continued pressure to automate repetitive welding tasks. The American Welding Society’s workforce analysis also projects a need for about 330,000 new welding professionals in the United States by 2028. Automation may address capacity, but not every line needs the most complex machine. In practice, rail length, joint access, plate thickness, and fixture accuracy should guide selection. I would validate these assumptions through production trials. Small alignment errors can expose large design weaknesses.

2026 Top Column And Boom Welding Machine Types? - Fixed, Traveling, Rotating, and Tandem-Arc Machine Configurations
Typical engineering ranges for column-and-boom welding systems. Actual specifications depend on workpiece size, welding process, duty cycle, automation level, and safety requirements.
Machine Configuration Primary Motion Typical Boom Reach Typical Vertical Travel Common Welding Processes Suitable Workpieces Main Advantages Key Limitations Typical Applications
Fixed Column and Boom Column remains stationary; the boom moves vertically and horizontally over the work area. Approximately 1.5–6 m Approximately 1.5–5 m Submerged arc welding (SAW), gas metal arc welding (GMAW), flux-cored arc welding (FCAW) Large components positioned on a stationary fixture, rotator, or welding positioner Rigid structure, good positional accuracy, high load capacity, and straightforward integration with existing fixtures Limited coverage unless the workpiece or fixture provides additional rotation or movement Pressure vessels, longitudinal seams, structural frames, and heavy fabricated assemblies
Traveling Column and Boom The complete column-and-boom assembly travels along floor rails or a dedicated track. Approximately 2–8 m Approximately 2–6 m SAW, tandem SAW, GMAW, FCAW, and narrow-gap welding Long weldments, tanks, beams, ship sections, and components requiring extended longitudinal coverage Large working envelope, continuous seam welding, and efficient use of floor space for long components Requires accurately installed rails, additional floor space, and regular maintenance of the travel system Long cylindrical shells, wind-tower sections, bridge components, rails, and heavy structural fabrication
Rotating Column and Boom The boom rotates around the column, usually together with vertical and horizontal boom movement. Approximately 2–6 m Approximately 2–5 m SAW, GMAW, FCAW, and mechanized overlay welding Workpieces arranged around a central operating area or components with multiple circumferential weld locations Access to several welding positions without relocating the workpiece; flexible coverage within a defined radius Rotational range and payload are constrained by the column structure, foundation, and cable-management system Pressure-vessel circumferential seams, tanks, pipe assemblies, and multi-position fabrication cells
Tandem-Arc Column and Boom Uses two coordinated welding arcs, commonly arranged in a tandem SAW configuration, on a fixed or traveling platform. Approximately 2–8 m, depending on the supporting configuration Approximately 2–6 m, depending on the supporting configuration Tandem SAW, twin-wire SAW, and selected multi-wire submerged arc processes Long, thick, and repetitive weld seams where high deposition productivity is required Higher deposition rate and travel speed than a single-wire setup when welding conditions are properly controlled Higher equipment cost, greater heat input, more complex parameter control, and stricter fit-up requirements Heavy plate fabrication, wind-tower production, shipbuilding, large pressure vessels, and long structural seams
Fixed Column with Rotating Positioner The column and boom remain fixed while a powered positioner rotates or tilts the workpiece. Approximately 1.5–5 m Approximately 1.5–4 m SAW, GMAW, FCAW, and robotic or mechanized welding processes Cylindrical parts, flanges, rings, pipe sections, and assemblies that benefit from downhand welding Improves weld-position control, reduces manual repositioning, and supports consistent circumferential welds Positioner capacity, workpiece diameter, and fixture design limit the usable range Pipe spools, vessel heads, nozzle connections, rings, and circular structural components

Key Specifications: 1–6 m Boom Travel, Duty Cycle, and Welding Speed

In 2026, column and boom welding machines are often judged by boom length. Travel range matters only when it matches weld geometry. A 1-meter boom suits compact frames and short seams. A 6-meter boom supports large tanks, beams, and long structural joints. Measure joint locations before choosing equipment. Leave room for torch angle and flux recovery. Small oversights create rework.

Boom travel should be smooth and controllable, not merely long. In practical shop testing, operators often reduce speed near corners, tack points, and thickness changes. A machine rated for 1–6 m travel should maintain stable motion across its working range. Check acceleration, positioning accuracy, and return repeatability. These details influence arc starts and seam alignment. The specification sheet may look impressive. The floor test matters more.

Duty cycle shows how long the machine can weld within a stated period, at a defined current and temperature. A high percentage supports long seams, but it does not guarantee high output. Welding speed must match wire feed, heat input, joint preparation, and cooling time. For example, 0.6 m/min may suit a thick structural seam, while thinner plate may require faster movement. Record actual arc-on time. Operators sometimes trust nominal speed too much. That mistake deserves review. Compare rated duty cycle with real shifts, including pauses, repositioning, and maintenance.

Selecting Machines for Tanks, Pressure Vessels, Wind Towers, and Steel Frames

2026 Top Column and Boom Welding Machine Types?

Selecting Machines for Tanks, Pressure Vessels, Wind Towers, and Steel Frames

For 2026 procurement, column and boom welding machines should match joint geometry, plate thickness, and production rhythm. The World Steel Association reported approximately 1.88 billion tonnes of crude steel production in 2024. Meanwhile, the Global Wind Energy Council recorded 117 GW of new wind capacity that year. These figures point to continued demand for repeatable welding in towers, vessels, and structural assemblies.

Tanks and pressure vessels usually benefit from fixed or traveling columns with rotators. Submerged arc welding supports long circumferential seams, while automatic voltage control helps maintain a stable arc. Pressure-vessel shops should verify procedure qualification, heat input limits, and traceability under ASME Section IX or ISO 3834 practices. Wind-tower production needs long boom travel, heavy-duty rotators, and reliable flange alignment. Steel-frame fabrication often needs a flexible traveling gantry and quick positioning for varied beam sizes. A larger boom is not always better. It may reduce access around stiffeners.

Tips: Measure the largest weld envelope, not only the vessel diameter. Check boom rigidity under load. Confirm torch oscillation, seam tracking, emergency stops, and maintenance access. Run a sample weld using actual plate thickness and joint preparation. Fit matters. One overlooked issue is operator visibility; poor sightlines can create rework, even with advanced automation. Review cycle-time data after the trial, not just the machine specification.

FAQS

How are column-and-boom welding machines classified?

They are commonly grouped by boom reach and load capacity. Light-duty machines reach about 2–4 meters and carry 250–500 kilograms. Medium-duty units reach 4–8 meters and carry 500–2,000 kilograms. Heavy-duty models may reach 8–12 meters and carry 2–10 tonnes. These boundaries are not exact.

Which machine suits tanks and medium fabrication cells?

A light-duty machine often suits tanks, beams, and medium fabrication cells. It can provide adequate torch access without excessive floor requirements. Check the actual weld envelope around nozzles and stiffeners. A simple size estimate may still miss awkward corners.

What equipment is suitable for long vessels?

Medium-duty equipment usually fits longer vessels and automated circumferential welding. A traveling column and a rotator can maintain steady joint positioning. Submerged arc welding may support long, continuous seams. The setup must match plate thickness and joint preparation.

What should pressure-vessel fabricators verify?

They should verify welding procedures, heat-input limits, and material traceability. Automatic voltage control can help maintain a stable arc. The machine should support documented quality practices and repeatable settings. A trial weld reveals problems that specifications may hide.

What machines work well for wind-tower production?

Wind-tower production often needs long boom travel and heavy-duty rotators. Reliable flange alignment is important for large circular sections. The foundation must handle machine loads and repeated movement. A long boom is useful, but vibration may increase.

What should steel-frame fabricators consider?

Steel-frame shops often benefit from traveling gantries and quick positioning. The machine should handle different beam sizes and changing weld locations. Fast repositioning can reduce idle time between joints. However, flexibility may reduce rigidity. That trade-off deserves testing.

Does a longer boom always improve productivity?

No. A longer boom can reduce repositioning and improve access across large assemblies. It may also increase vibration, deflection, and alignment errors. Measure torch movement under real load. Reach alone is not productivity.

How should buyers check the rated load capacity?

Ask whether the rating includes only the carriage and torch. It may exclude the workpiece, fixture, or additional tooling. Request load charts and tested deflection data. Review foundation calculations for the actual installation site. This detail is easy to overlook.

What should be tested before purchasing?

Run a sample weld using the intended plate thickness and joint preparation. Check vertical travel, torch oscillation, seam tracking, and emergency stopping. Inspect operator visibility and maintenance access. Record cycle time after the trial. The first trial may expose an inconvenient weakness.

Conclusion

In 2026, Column And Boom Welding Machine systems are classified mainly by boom reach, load capacity, travel design, and welding performance. Common configurations include fixed, traveling, rotating, and tandem-arc machines, allowing manufacturers to match equipment with different workpiece sizes and production requirements. Boom travel typically ranges from 1 to 6 meters, while load capacity and duty cycle determine how reliably the machine can handle extended welding operations.

Submerged arc systems can be compared by deposition rates of approximately 5–15 kg/h, depending on the welding method, wire arrangement, and operating conditions. Important specifications also include welding speed, positioning accuracy, control functions, and compatibility with automated flux and wire delivery. For tanks and pressure vessels, stable travel and precise positioning are essential; wind towers may require greater reach and high productivity, while steel frames often benefit from flexible rotation and adaptable load handling. Selecting the right machine requires balancing component dimensions, weld volume, production speed, and required operating continuity.
Ethan

Ethan

Ethan is a seasoned marketing professional with a deep expertise in our company's innovative product line. With a passion for sharing knowledge and insights, he takes the lead in regularly updating our corporate blog, where he explores industry trends, product features, and effective marketing......